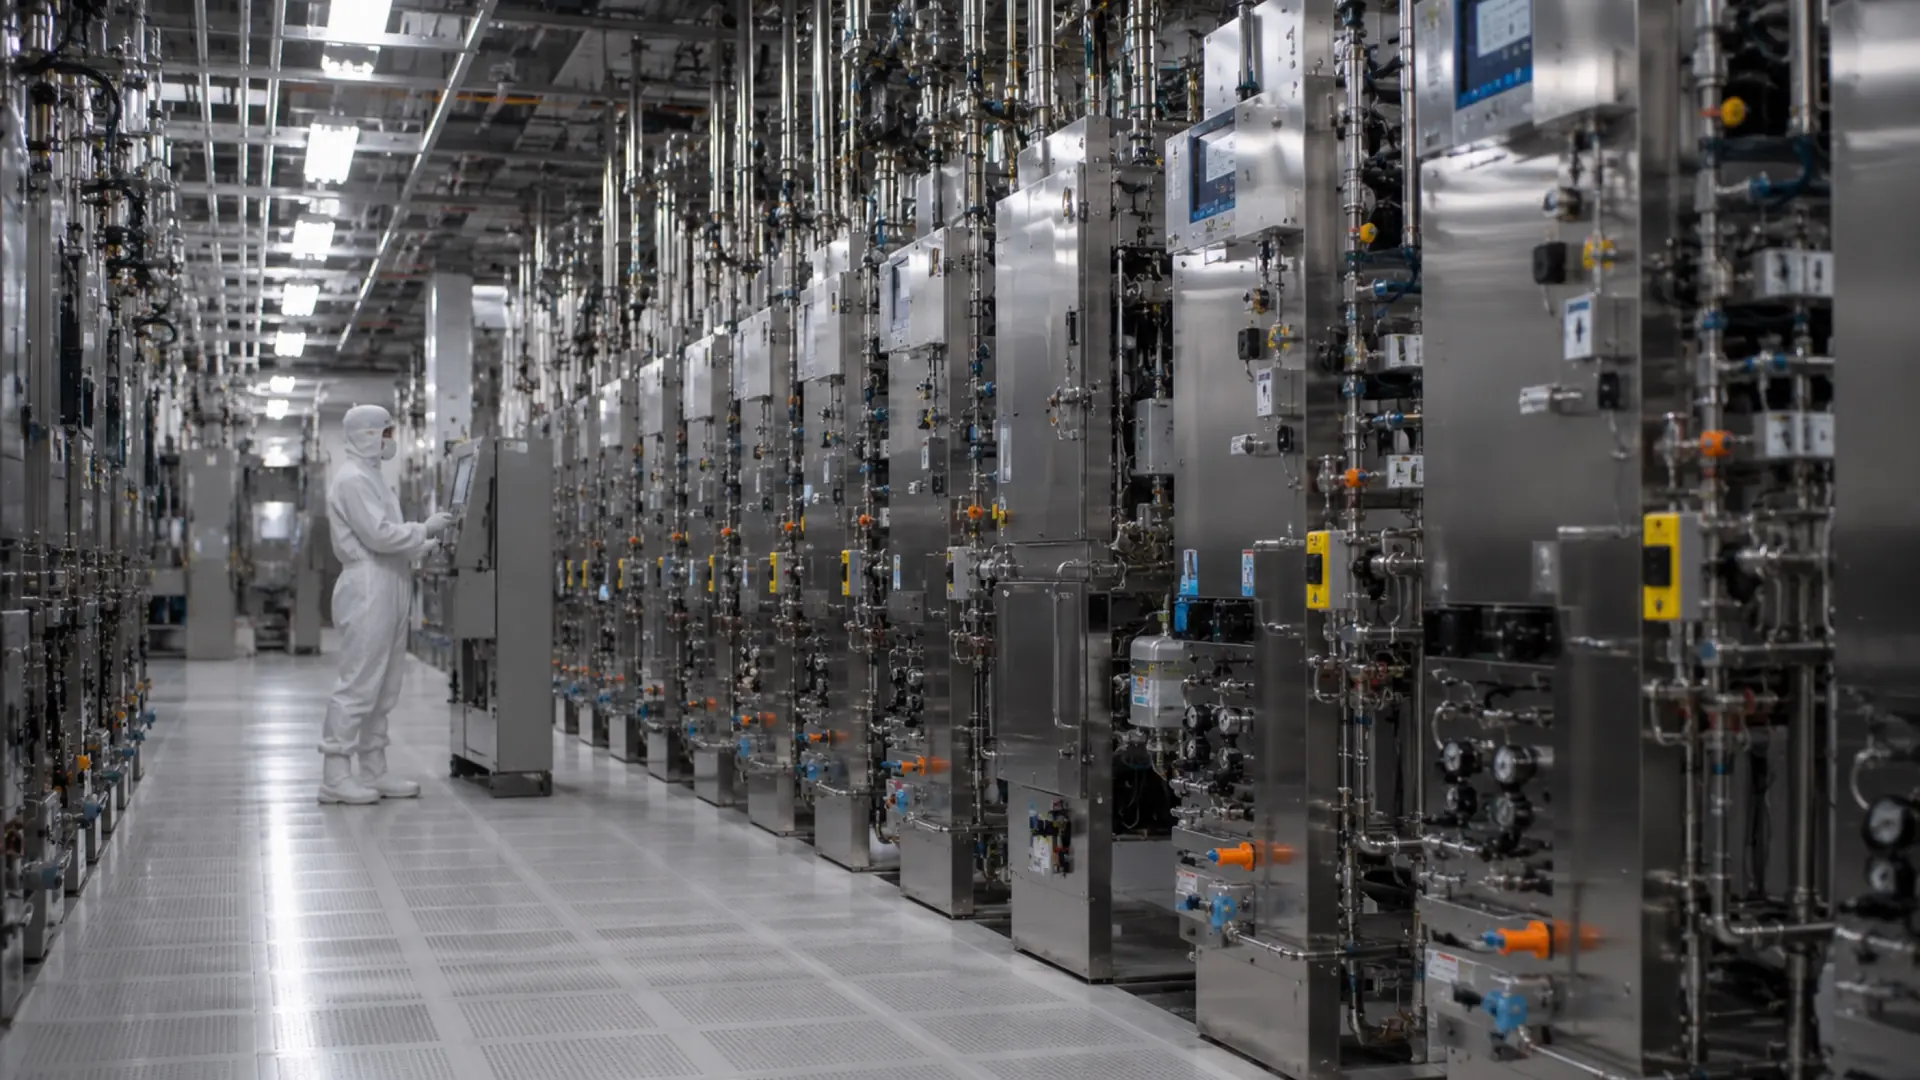
In a semiconductor wafer fab, the sub-fab and utility levels run thousands of lines carrying pyrophoric, toxic, and corrosive specialty gases and ultra-high-purity chemicals.
Managing visual and boroscopic weld inspections, helium leak tests, double-containment sensor checks, and exhaust-duct fireproofing across tool hookups and annual facility shutdowns had outgrown disconnected contractor binders.
Current state before intelliSPEC
- Scattered tool-hookup quality packs: High-purity orbital weld logs, borescope videos, and pressure-test certificates from contractor crews lived in project turnover folders rather than on the valve manifold box (VMB) or gas cabinet asset record.
- High-stakes shutdown coordination: During the annual total-facility power-down, hundreds of gas-line tie-ins, scrubber inspections, and life-safety checks had to be verified before re-energizing and introducing process gases.
- Manual hazardous-production-material (HPM) audits: Proving compliance with NFPA 318, SEMI S2, and local fire-code containment rules required cross-referencing P&IDs against spreadsheet logs.
Configured path
The fab implemented intelliVISION, intelliINSPECT, intelliNDT, intelliPROJECTS, and intelliCOMPLY, with sub-fab execution on intelliEDGE.
- Line-to-VMB asset spine: Gas cabinets, VMBs, double-containment chemical lines, and abatement scrubbers were mapped in
with DEXPI-aligned P&ID tag relationships. - Digital weld and leak-test capture: Hookup and NDE crews logged borescope media, purge parameters, and leak-test results per weld in
and. - Gated annual power-down:
managed the facility shutdown wall chart, requiring signed LOTO, leak-test, and life-safety verification inbefore any system cleared its restart gate.
Measured outcome
- On-schedule fab restart: Every gas and chemical tie-in cleared its restart gate with a verified leak test and engineer signature visible on the command screen.
- Permanent weld traceability: Clicking any VMB or sub-fab line retrieves its original orbital weld log, borescope image, and subsequent inspection history.
- Clean NFPA 318 and insurer reviews: Containment, exhaust, and HPM inspection trails export on demand.