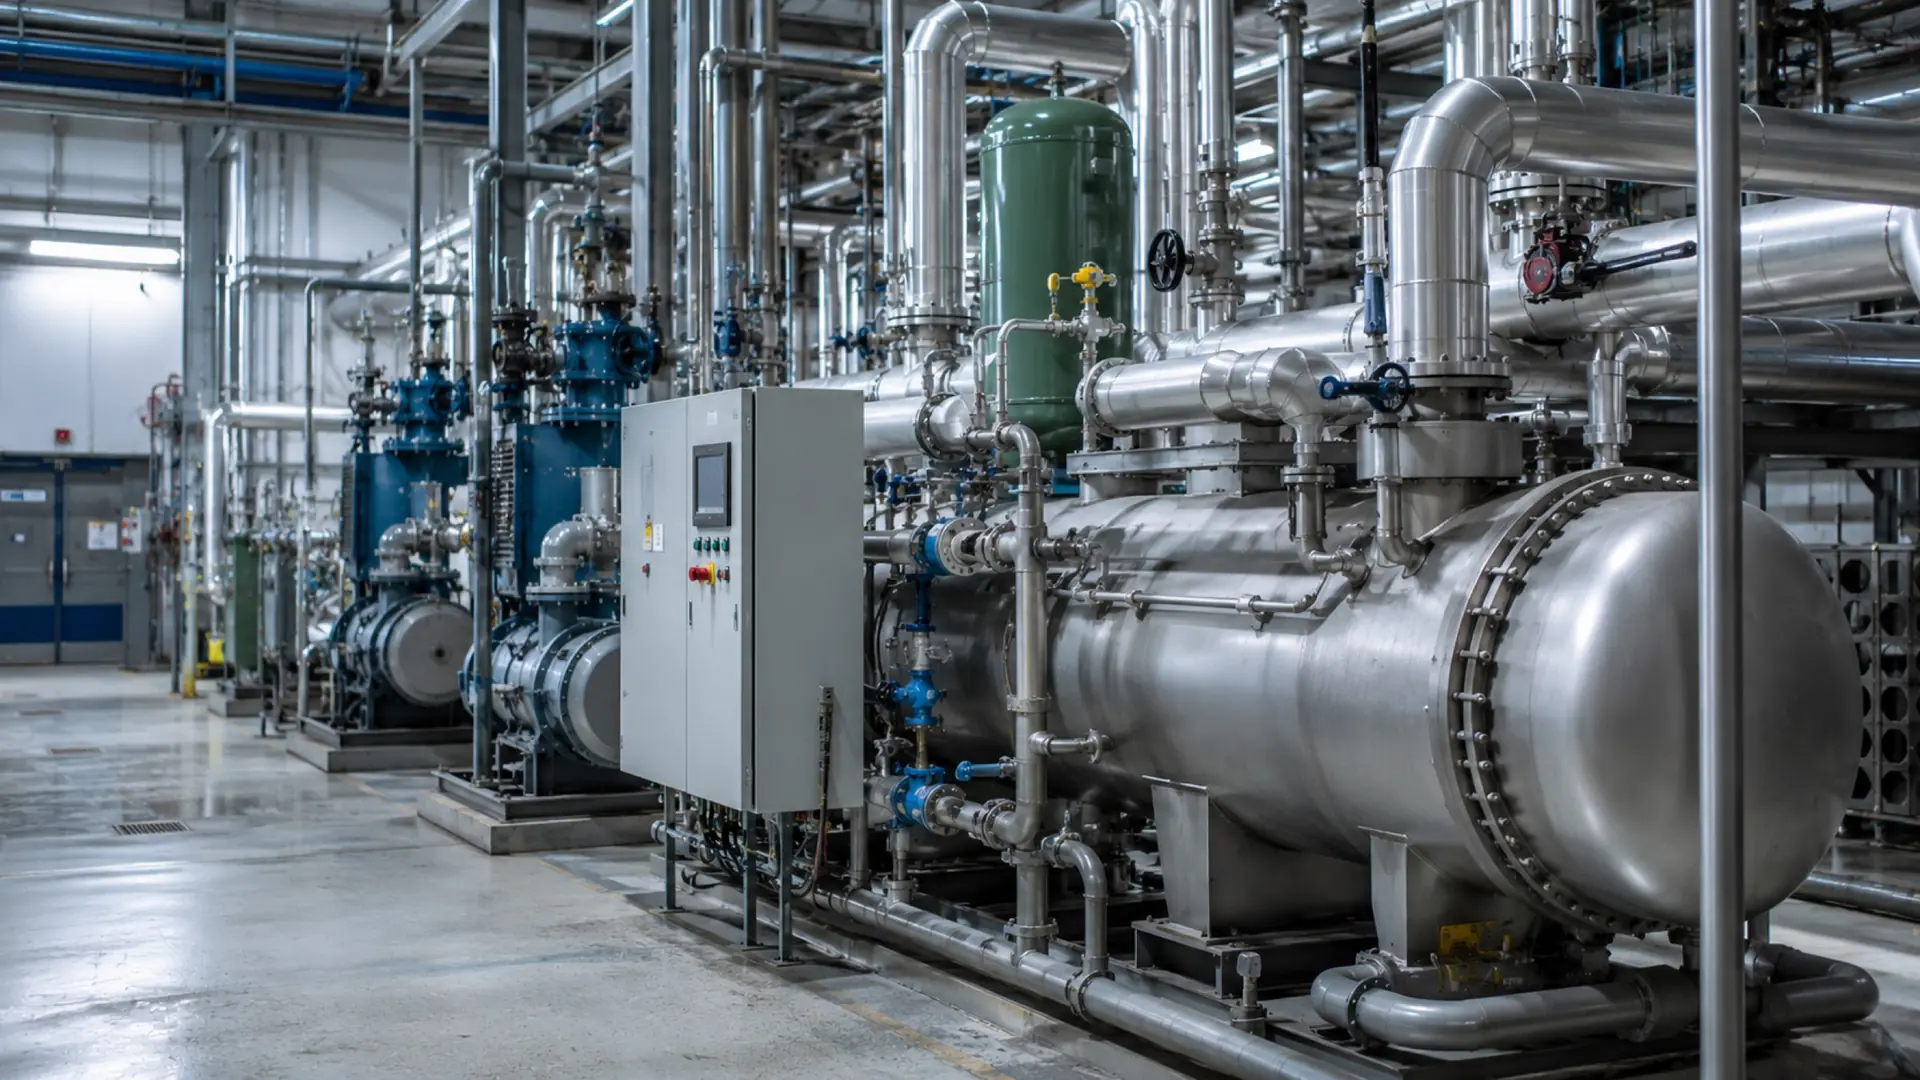
A food and beverage manufacturer operating anhydrous ammonia refrigeration systems above the 10,000-pound OSHA Process Safety Management (PSM) and EPA Risk Management Plan (RMP) threshold across multiple plants needed a consistent way to manage ANSI/IIAR 6 inspections, corrosion under insulation (CUI) on low-temperature suction lines, and pressure-relief valve (PRV) replacement intervals.
Current state before intelliSPEC
- Plant-by-plant binder systems: Each facility kept its own IIAR checklists, daily compressor logbooks, and five-year mechanical integrity audit reports in local ring binders.
- Hidden CUI on vapor-barrier breaches: Ice buildup and damaged vapor barriers on insulated ammonia piping were noted in walkdown emails, but ultrasonic wall-thickness follow-up was rarely linked back to the line segment.
- Manual PRV five-year swaps: Tracking dual-relief-valve manifold tag numbers, installation dates, and five-year replacement deadlines across roofs and engine rooms relied on fragile spreadsheets.
Configured path
The processor deployed intelliVISION, intelliINSPECT, intelliNDT, intelliINTEGRITY, and intelliCOMPLY, with roof and freezer-room capture on intelliEDGE.
- Engine-room-to-evaporator register: High-pressure receivers, thermosyphon vessels, evaporative condensers, ammonia pumps, evaporator coils, and PRVs were registered in
per plant. - IIAR 6 guided workflows offline: Operators and third-party inspectors ran IIAR 6 checklists and CUI visual/UT walks on
tablets inside -20 F blast freezers and on penthouse roofs with no Wi-Fi. - Closed-loop deficiency governance: Any frost-heave, vapor-barrier failure, or pitted ammonia line opened a tracked corrective action in
with engineering sign-off.
Measured outcome
- Standardized PSM / RMP evidence: Corporate EHS and plant engineers view real-time IIAR 6 inspection status, PRV expiry dates, and open mechanical-integrity actions across every facility.
- Targeted insulation repair: Ultrasonic thickness trends and CUI flags identify which low-temp ammonia lines need insulation stripping and recoating before wall loss becomes critical.
- Zero overdue relief valves: PRV serials and five-year changeout dates are tracked on the vessel and manifold record.