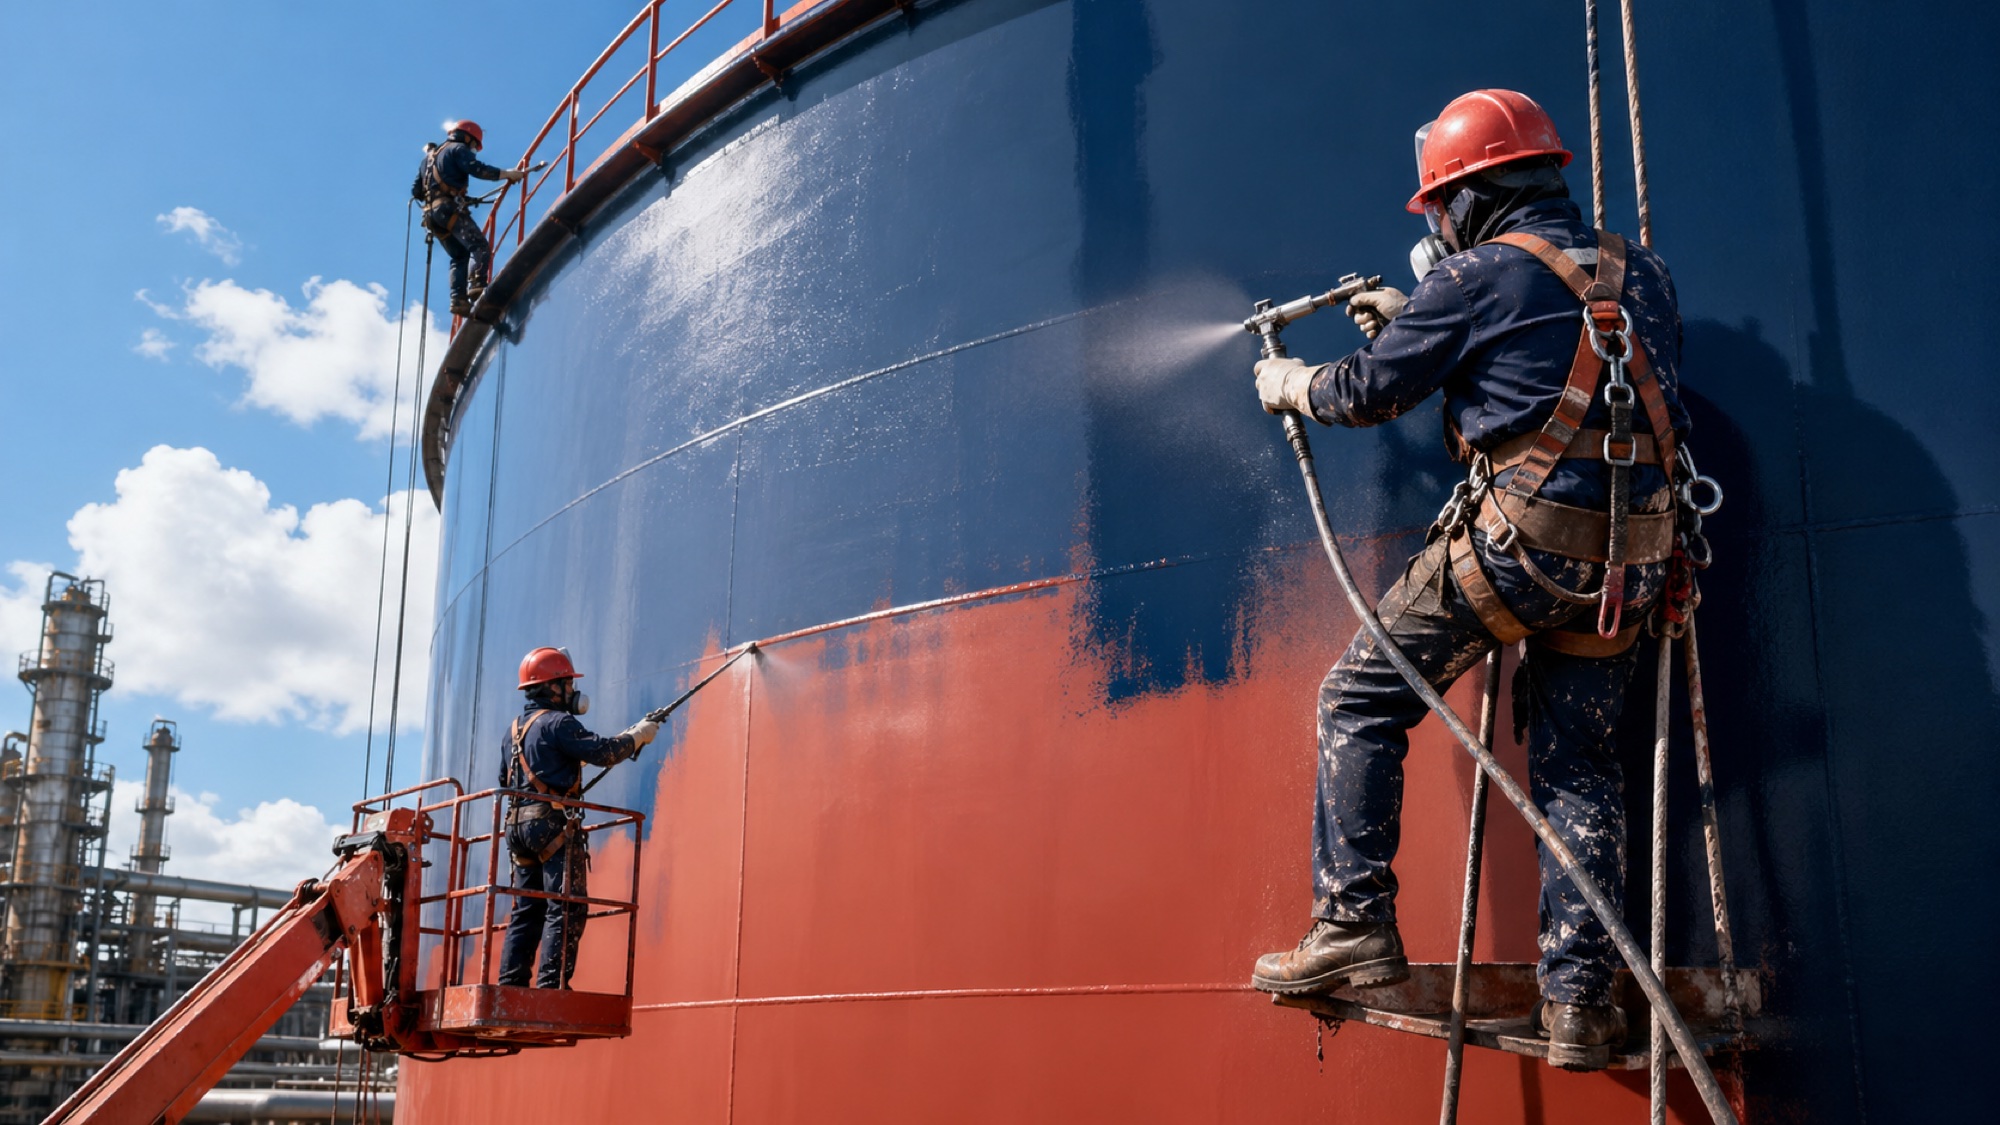
Most premature coating failures are not product failures. They are process failures that happened weeks before anyone opened a can: a surface profile that was never measured, a dew point margin that was assumed, a recoat window that closed overnight. Hold points exist to force verification at the moments where a defect becomes unrecoverable, and an AMPP certified coating inspector is trained to treat them as gates, not suggestions.
The gates, in order
A typical industrial coating specification builds hold points around the same sequence, because the physics does not change from job to job.
Pre-surface preparation
- Ambient conditions. Air temperature, surface temperature, relative humidity, and dew point, with the standard margin between surface temperature and dew point verified before blasting starts, not after.
- Compressed air cleanliness. A blotter check confirming the air feeding the blast pot is free of oil and moisture. Contaminated air embeds the problem under everything that follows.
After surface preparation
- Cleanliness grade. Visual comparison against the specified preparation standard, with the inspector, not the blaster, making the call.
- Surface profile. Measured, usually with replica tape or a depth gauge, and recorded per area. Profile outside the primer's specified range is a re-blast, and this is the hold point crews most want to negotiate.
- Soluble salts. Where the spec requires it, a conductivity test with the numeric result recorded. "Looked clean" is not a result.
During application
- Environmental re-checks. Conditions drift across a shift. A morning reading does not cover an afternoon coat.
- Wet film thickness. Checked as the applicator works, because it is the only thickness reading that can still change the outcome.
- Recoat windows. Minimum and maximum intervals per the product data sheet, with actual times logged, not recalled.
After each coat and at final
- Dry film thickness. Gauge readings taken per the sampling standard the spec invokes, recorded individually, not as one averaged number.
- Holiday detection on immersion and buried service, with the test voltage recorded.
- Cure verification and final visual for runs, sags, pinholes, and dry spray before the system is accepted.
Why the record is the fight
Here is the uncomfortable part. When a coating fails in year two of a ten-year system, the dispute is contractual, and it is settled entirely on the daily inspection records. The applicator says conditions were in spec. The owner says the profile was never verified. Whoever has the dated, signed, per-area readings wins. An inspector's logbook that says "conditions OK" loses to one that says "surface 61 F, dew point 48 F, 0900, west wall, gauge serial recorded."
That is why experienced inspectors are pedantic about capture at the hold point itself. A reading transcribed at the trailer that evening is already a reconstruction, and reconstructions are where numbers drift and coverage gaps hide.
intelliPAINT, the coatings module in intelliSPEC, structures the job around these gates: each hold point captures its readings, photos, and sign-off in sequence, and the daily log assembles as the crew works. If your coating records still live in a rite-in-the-rain notebook, bring a recent job's spec to a demo and walk it through.